Why This Comparison Matters for Indian Plant Managers
Every year, plant heads and operations directors across Gujarat, Maharashtra, and Rajasthan face the same decision: we know we need to improve — but which methodology do we start with?
The wrong answer costs more than time. Choose Six Sigma when you need 5S first, and your trained Black Belts will be solving statistical problems on a shop floor where tools go missing, and nobody knows the standard process. Choose TPM when your real problem is overproduction and inventory bloat, and you will spend 18 months on machine checklists while your working
capital sits locked in raw material.
The question is not which methodology is best. The question is which methodology is right for your plant, at this moment in its improvement journey.
This guide will help you answer that — with honesty about what each framework can and cannot do, what it costs in time and resources, and how Indian SMEs with 50 to 500 employees typically deploy these tools.
Disclosure: GreenDot Management Solutions has implemented TPM, Lean, and hybrid frameworks across manufacturing plants in Gujarat, Maharashtra, and Rajasthan for over 25 years. The observations in this article draw from that field experience.
What “Maximum ROI” Actually Means in Indian Manufacturing
Before comparing frameworks, it is worth agreeing on what ROI means in this context, because it is not just a cost-cutting number.
For a mid-size manufacturer, ROI from a continuous improvement programme typically shows
up in five places:
- Uptime recovery — Every unplanned breakdown hour has a cost. For a machine producing ₹50,000 of output per shift, even one hour of daily downtime costs ₹15–18 lakh per year in lost production.
- Quality cost reduction — Rework, scrap, and customer rejections are not just material costs. They consume operator time, machine capacity, and management attention. The Cost of Poor Quality (COPQ) in Indian manufacturing plants typically runs between 5% and 15% of turnover — often invisible because it is never measured as a single number.
- Space and inventory recovery — Freed floor space is productive capacity. Reduced WIP frees working capital.
- Labour productivity — Operators doing value-adding work instead of searching for tools, waiting for materials, or fixing recurring machine problems.
- Employee engagement — Often underestimated. Plants with structured improvement programmes consistently report lower attrition, particularly among skilled operators and technicians.
TPM — Total Productive Maintenance
What It Is
TPM was developed at Nippondenso, a Toyota supplier, in 1971 and is built around a single insight: equipment reliability is everyone’s responsibility, not just the maintenance department’s.
The framework is structured around 8 Pillars:
| Pillar | Focus |
|---|---|
| Jishu Hozen (Autonomous Maintenance) | Operators maintain their own machines |
| Keikaku Hozen (Planned Maintenance) | Scheduled maintenance based on failure history |
| Kobetsu Kaizen (Focused Improvement) | Eliminating specific recurring losses |
| Hinshitsu Hozen (Quality Maintenance) | Preventing quality defects through machine conditions |
| Safety, Health & Environment | Zero accidents on the shop floor |
| Education & Training | Building skills for operators and maintenance teams |
| Office TPM | Streamlining administrative processes |
| Early Equipment Management | Designing reliability into new equipment from day one |
In practice, most Indian plants deploying TPM for the first time focus on the first three pillars: autonomous maintenance, planned maintenance, and focused improvement.
The Core Metric: OEE
TPM measures progress through Overall Equipment Effectiveness (OEE):
OEE = Availability × Performance × Quality
- Availability: How often is the machine actually running vs. planned?
- Performance: When running, is it operating at rated speed?
- Quality: Of what it produces, how much is good first time?
World-class OEE is considered 85%. Indian manufacturing plants — depending on sector — typically measure between 45% and 65% when they first start tracking. That gap represents recoverable capacity that requires no new capital investment.
What TPM Delivers
| Benefit | What It Delivers |
|---|---|
| Reduction in unplanned breakdowns | Plants in GreenDot’s programme have achieved 40–70% breakdown reduction in the first 12 months |
| Increased machine availability | The most direct path to higher output without buying new equipment |
| Operator ownership of machine condition | A cultural shift that helps sustain gains |
| Safer workplace | Standardised inspection and cleaning routines improve workpl |
What TPM Does Not Do
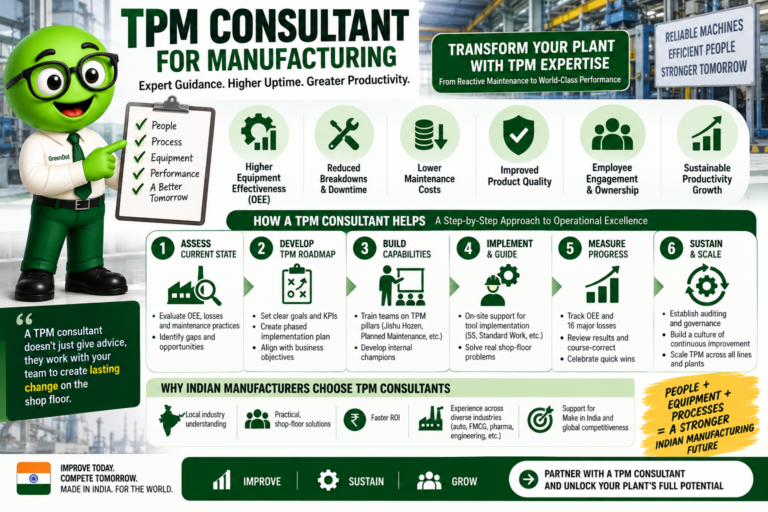
TPM does not fix process flow problems. If your scheduling is chaotic, your material supply is erratic, or your changeovers take four hours, TPM will improve your machine but not your system. Those problems need Lean.
TPM also does not reduce statistical variation in your process output. If you have a dimensional tolerance problem driven by process capability, that requires Six Sigma.
Best Suited For
TPM is best suited for asset-intensive industries where machine reliability directly determines output, including:
- Chemical plants
- Pharmaceutical manufacturers
- Engineering and casting units
- Plastics processors
- FMCG production lines
- Packaging plants
Typical investment: 12–24 months to sustained results.
First visible improvements: Breakdown reduction, cleaner machines, and an OEE baseline can typically become visible within 90 days.
Lean Manufacturing
Lean comes from the Toyota Production System (TPS), developed in post-war Japan and documented for the Western world in the 1990 book The Machine That Changed the World. Its core principle: eliminate everything that consumes resources without adding value for the customer.
The 8 Types of Lean Waste — TIMWOODS
| Waste | What It Looks Like in a Plant |
|---|---|
| Transport | Moving materials unnecessarily between locations |
| Inventory | Raw material, WIP, or finished goods beyond what is needed |
| Motion | Operators walking, bending, or reaching more than necessary |
| Waiting | People or machines idle, waiting for materials, approvals, or the next process |
| Overproduction | Making more than what the customer currently needs |
| Overprocessing | Steps in the process that do not add value for the customer |
| Defects | Rework, scrap, and correction of mistakes |
| Skills (Unused Talent) | Ideas, knowledge, and capability that goes untapped |
Key Lean Tools
5S is almost always the starting point — Sort, Set in Order, Shine, Standardise, Sustain. It creates a clean, organised, visual workplace where waste and abnormalities become immediately obvious. It is a prerequisite for almost everything else.
Beyond 5S, the Lean toolkit includes:
- Value Stream Mapping (VSM): Map the entire production flow to identify where time and value are being lost.
- Kaizen: Structured small-group problem solving for continuous incremental improvement.
- SMED (Single Minute Exchange of Die): Reducing changeover time to increase flexibility.
- Kanban: Visual pull systems to control WIP and inventory.
- Poka-Yoke: Mistake-proofing devices to prevent defects at the source.
What Lean Delivers
- Fast, visible improvements — 5S results are visible within weeks, not months.
- Floor space recovery — commonly 10–25% of total floor area in early 5S projects.
- Working capital release through inventory reduction.
- Shorter lead times and better on-time delivery.
- A culture of problem visibility — waste becomes something people notice and fix.
What Lean Does Not Do
Lean does not provide a framework for equipment reliability. A 5S programme does not prevent breakdowns. Kanban does not reduce machine cycle time variation. For asset-intensive plants, Lean prepares the foundation but TPM must follow.
Lean also does not use statistical tools to address process capability problems. Persistent quality variation requires Six Sigma’s data-driven approach.
Best Suited For
Any operation where waste, flow, inventory, and speed are the primary problems. Lean is the most versatile framework and often the right starting point — even in plants that will eventually need TPM or Six Sigma.
Typical investment: 1–3 months for first visible results from 5S. Lead time reduction and flow improvements take 6–12 months of sustained Kaizen activity.
Six Sigma
Six Sigma was developed at Motorola in 1986 and popularised globally by GE’s Jack Welch in the 1990s. It uses statistical methods to reduce variation in processes — aiming for no more than 3.4 defects per million opportunities (the “six sigma” level of quality).
DMAIC Methodology
Six Sigma projects follow the DMAIC methodology:
| Phase | What Happens |
|---|---|
| Define | Define the problem, customer requirements, and project scope |
| Measure | Collect data on the current process and establish a baseline |
| Analyse | Identify the root causes of variation and defects |
| Improve | Design and implement solutions |
| Control | Put controls in place to sustain the improvement |
What Six Sigma Delivers
- Consistent, measurable reduction in defects and process variation
- Data-driven decision making — problems are proven, not assumed
- Reduced Cost of Poor Quality (COPQ) — less scrap, rework, and customer complaints
- Improved process capability (Cpk) — the ability to consistently meet specification
What Six Sigma Does Not Do
Six Sigma does not organise your workplace, reduce machine downtime, or improve flow. It is a precision tool for persistent quality problems that have been measured and are understood to be significant. Applying Six Sigma to a plant that has not yet stabilised its processes with Lean and TPM typically produces studies, not results.
Six Sigma also requires significant skill investment. Green Belt and Black Belt training takes months. For many Indian SMEs with limited training budgets, this is a real constraint.
Best Suited For
Pharmaceutical, electronics, aerospace, automotive OEM suppliers, and food processing — industries where customer specifications are tight, consequences of defects are serious, and the investment in statistical analysis is justified by the cost of failure.
Typical investment: 6–12 months per DMAIC project. A plant typically runs 2–4 Six Sigma projects per year once the methodology is established.
The Full Comparison: TPM vs Lean vs Six Sigma
| Criteria | TPM | Lean Manufacturing | Six Sigma |
|---|---|---|---|
| Primary Goal | Equipment uptime & reliability | Waste elimination & flow | Defect reduction & process control |
| Equipment Uptime & Reliability | ★★★★★ | ★★☆☆☆ | ★★☆☆☆ |
| Waste Elimination & Flow | ★★☆☆☆ | ★★★★★ | ★★☆☆☆ |
| Breakdown Reduction | ★★★★★ | ★★☆☆☆ | ★☆☆☆☆ |
| Quality Improvement | ★★★☆☆ | ★★★☆☆ | ★★★★★ |
| Cost Reduction | ★★★★☆ | ★★★★☆ | ★★★★☆ |
| Space & Inventory | ★★☆☆☆ | ★★★★★ | ★★☆☆☆ |
| Speed of First Results | Medium (3–6 months) | Fast (1–3 months) | Slow (6–12 months) |
| Employee Engagement | ★★★★☆ | ★★★★★ | ★★★☆☆ |
| Skill Requirement | Very High | Moderate | High |
| Statistical Tools Required | No | No | Yes |
| Sustains Without Leadership | No (needs daily discipline) | No (needs daily discipline) | Partially (control phase) |
| Minimum Plant Size | 30+ operators | Any size | 100+ employees recommended |
| Typical MSME Entry Point | After 5S is established | First step | After Lean + TPM are stable |
Which Framework Is Right for Your Plant?
Use this decision guide based on your primary pain point:
| Your Biggest Problem Right Now | Recommended Starting Framework |
|---|---|
| Machines breaking down frequently, unplanned downtime eating output | TPM — start with OEE measurement and Jishu Hozen |
| Shop floor is cluttered, processes unclear, high WIP | Lean (5S first) — organise before optimising |
| Products failing customer specifications, high rework and rejection | Six Sigma — after you have baseline data |
| High inventory, long lead times, late deliveries | Lean (VSM + Kanban) |
| Low operator morale and engagement, no ownership culture | Lean (Kaizen teams) |
| Want a long-term transformation, not a one-time project | Hybrid: Lean → TPM → Six Sigma |
| Small plant (under 50 people), limited budget | Lean (5S + Kaizen) — highest ROI per rupee at this scale |
| Already doing 5S, ready for the next level | TPM |
A Note for Indian MSMEs Specifically
Many global articles recommend starting with Six Sigma. For Indian SMEs with 50–300 employees, this is rarely the right advice. Here is why:
Six Sigma requires a stable process to measure. Most SMEs have not yet standardised their processes. Six Sigma also requires trained practitioners (Green Belts, Black Belts) — an investment that makes sense once the bigger structural wastes are already removed.
In GreenDot’s experience across 25+ years and hundreds of plants in Gujarat and Maharashtra, the sequence that works for Indian SMEs is almost always:
5S → Kaizen → TPM → Six Sigma
Each stage creates the foundation the next stage needs.
The Hybrid Approach: Integrating All Three
The best results come from combining frameworks strategically. Here is a realistic integration roadmap for an Indian manufacturing plant:
| Phase | Framework | Timeframe | Key Activities | Goal |
|---|---|---|---|---|
| Phase 1 — Foundation | Lean | Months 1–6 | Implement 5S across the shop floor; map the value stream (VSM) to identify the biggest time and waste losses; launch first Kaizen events on the top 3 wastes; establish visual management and daily team meetings | Clean, organised, visible workplace with teams engaged in improvement |
| Phase 2 — Reliability | TPM | Months 6–18 | Baseline OEE on the top 3 machines by output value; train operators in Jishu Hozen (autonomous maintenance); build Planned Maintenance schedules based on failure history; run Focused Improvement (Kobetsu Kaizen) on the top breakdown causes | Breakdown reduction of 40%+ and OEE improvement of 10–20 points |
| Phase 3 — Precision | Six Sigma | Months 18–36 | Identify the top recurring quality defects by COPQ; train 2–3 team members as Six Sigma Green Belts; run structured DMAIC projects on the highest-value problems | Defect reduction to Cpk ≥ 1.33 on key parameters |
| Phase 4 — Digital & Sustained | Industry 4.0 Integration | Ongoing | Add real-time OEE monitoring using IoT sensors on machines; introduce predictive maintenance triggers based on machine data; create dashboard visibility for production, quality, and maintenance KPIs | Shift from reactive to predictive operations |
Also Worth Knowing: TPM vs Preventive Maintenance vs Predictive Maintenance
Many plant managers use these terms interchangeably. They are not the same:
| Criteria | Preventive Maintenance | Predictive Maintenance | TPM |
|---|---|---|---|
| Who Does It | Maintenance department only | Maintenance with sensor data | Operators + maintenance team together |
| Trigger | Time-based schedule (every X hours) | Condition-based (when data says so) | Condition-based + daily inspection |
| Operator Role | None | None | Central (Jishu Hozen) |
| Equipment Knowledge | Maintenance team only | Maintenance + data systems | Shared across all operators |
| Cost | Medium (scheduled work) | High (sensor investment) | Medium (training investment) |
| Culture Change | Low | Medium | High |
| Best for Indian SMEs | Good starting point | Requires digital infrastructure | Best long-term approach |
Case Study 1 — Lean (5S): VOXCO Pigments and Chemicals Pvt Ltd
VOXCO Pigments and Chemicals Pvt Ltd partnered with GreenDot when their shop floor had no SOPs, no standard tool storage, and no process for managing scrap. Audit scores were 9% — a number that is more common than most plant managers are willing to admit.
GreenDot implemented a structured 5S programme: workspace layout redesign, shadow boards for tools, standard scrap management, and team-led cleaning and inspection routines. Training was conducted in the local language to ensure shop floor adoption.
Results
| Measure | Result |
|---|---|
| 5S audit score | From 9% to 72% |
| Floor space recovered | 1,450 sq. ft. |
| Scrap systematically identified and sold | ₹3.2 lakh recovered |
| Employee participation in improvement activities | Significantly increased |
“The structured approach not only organised our shop floor but also boosted employee morale and efficiency.” — VOXCO Management
The lesson: 5S is not housekeeping. It is the first act of turning a workforce into problem-solvers. VOXCO’s improvement created the visual platform from which deeper improvements — equipment reliability, flow, quality — could be pursued.
Case Study 2 — TPM: New India Cuprotec (Engineering Sector)
New India Cuprotec, an engineering components manufacturer, engaged GreenDot to address persistent OEE losses on their production machines. Before the engagement, breakdowns were treated as normal — something to fix when they happened, not something to prevent.
GreenDot’s intervention focused on OEE measurement and the first three TPM pillars: autonomous maintenance (Jishu Hozen), planned maintenance scheduling, and focused improvement on the top three breakdown causes.
Results Achieved Through TPM Implementation
| Area | Result |
|---|---|
| Machine OEE | Improved measurably through the engagement period |
| Operator capability | Operators developed hands-on inspection skills they previously did not have |
| Maintenance activities | Maintenance team shifted time from emergency breakdown response to planned work |
Testimonial: Testimonial on file from New India Cuprotec (Coptec) — contact GreenDot for details.
The lesson: When operators understand and own their machines, breakdowns stop being surprises. The Jishu Hozen step — which many plants skip because it “takes too long” — is precisely the step that makes TPM results stick.
Common Mistakes When Choosing a Framework
After 25 years of implementation experience across Indian manufacturing, these are the mistakes GreenDot sees most often:
- Starting with Six Sigma before processes are stable.
Six Sigma measures variation. If your process changes every day based on who is on shift, what material arrived, and whether the machine is running well, you are measuring chaos — not process capability. Stabilise first.
- Implementing TPM without 5S as a foundation.
Clean, organised machines are a prerequisite for Jishu Hozen. Operators cannot spot abnormalities on a dirty, cluttered machine. 5S must come first.
- Treating these programmes as projects with end dates.
The most common reason Lean, TPM, and Six Sigma programmes fail is that they are run as projects. They are not projects. They are operating disciplines that require daily leadership attention indefinitely.
- Sending one or two people for training and calling it implementation.
Training creates knowledge. Implementation requires structured practice on the shop floor, with coaching, feedback, and accountability. These are not the same thing.
- Choosing the methodology based on what competitors are doing.
Your competitor’s plant is not your plant. Their biggest problem may be machine reliability; yours may be process flow. Choose based on a clear diagnosis of your actual constraint.
- Skipping the measurement baseline.
You cannot improve what you do not measure. OEE cannot be improved if you do not know your current OEE. COPQ cannot be reduced if you have never calculated it. The first investment in any programme is measurement.
What GreenDot’s Diagnostic Process Looks Like
Before GreenDot recommends any framework to a new client, we run a structured plant assessment. Here is what that involves:
Step 1: Shop Floor Walk
A structured Gemba walk to observe actual conditions — machine cleanliness, operator behaviour, visual management, WIP levels, and tool organisation.
Step 2: Data Collection
Where available, we review production records, maintenance logs, quality rejection data, and OEE history. Where data does not exist, we help establish it.
Step 3: Loss Identification
Using the Six Big Losses framework (for machines) and the 8 Wastes framework (for processes), we categorise where time, quality, and efficiency are being lost.
Step 4: Prioritisation
We map losses to their cost impact and identify the highest-value intervention point — which is not always the most obvious one.
Step 5: Recommendation
Only after steps 1–4 do we recommend a starting framework. The recommendation is always specific to the plant’s current maturity and resource capacity — not a generic answer.
Housekeeping focuses on physical cleanliness — sweeping, mopping, removing visible waste.
5S is a structured discipline system that covers organisation, waste elimination, equipment
inspection, process standardisation, and cultural change. Housekeeping is a task that gets done
periodically. 5S is a system that shapes how work happens every day. Under India's Factories
Act 1948, housekeeping is a legal minimum. 5S goes far beyond that minimum.
Six Sigma is valuable for any organisation with a measured, persistent quality problem worth
solving. However, the training investment (Green Belt, Black Belt certification) can be difficult
to justify for very small plants. For Indian SMEs under 200 employees, a focused Kaizen
approach to quality problems often delivers 80% of the benefit at 20% of the cost. Six Sigma
becomes fully worthwhile when Lean and TPM are already established and quality remains the
limiting factor.
Preventive maintenance is time-based maintenance done by the maintenance department. TPM is
a total system that includes operator-led daily care (Jishu Hozen), planned maintenance by the
maintenance team, and focused problem-solving on chronic losses. The biggest difference is
cultural: TPM makes every operator a partial maintainer of their machine.
In GreenDot's experience, the first measurable improvements — a reduction in daily
breakdowns, cleaner machines, an established OEE baseline — are visible within 60–90 days.
Significant OEE improvement (10–20 points) typically appears in months 6–12. Full financial
ROI depends on the plant's starting point and the cost of downtime, but plants typically recover
the consulting and training investment within the first year.
Yes — Lean, and specifically 5S and Kaizen, is arguably most effective in small plants. The
implementation is simpler, the team is smaller and more cohesive, and results are visible
immediately. GreenDot has implemented Lean in plants as small as 15–20 employees with
strong results.
The Government of India's National Manufacturing Competitiveness Programme (NMCP),
administered through the Ministry of MSME, has historically subsidised Lean Manufacturing
implementations for eligible MSME units. Schemes and eligibility criteria change; contact your
nearest MSME Development Institute (MSME-DI) or District Industries Centre (DIC) for
current details. GreenDot can assist clients in navigating these schemes where applicable.
Scheduled maintenance done by a maintenance department alone is Preventive Maintenance —
not TPM. The difference TPM makes is operator involvement. When operators perform daily
inspection and basic care (cleaning, lubrication, tightening), they detect abnormalities before
they become breakdowns. Studies from Toyota's supplier network consistently show that
operator-maintained machines have significantly higher OEE than maintenance-team-only
maintained machines. TPM does not replace your maintenance team — it makes them more
effective by catching problems earlier.
5S programmes fail for a predictable set of reasons: no daily audit discipline, no leadership
visibility, no consequence for non-compliance, and no integration into team leader routines. The
5S itself was not the problem — the sustainment system was missing. GreenDot's approach
builds the sustainment system (audit templates, daily checklists, scoring systems, leader standard
work) at the same time as the initial implementation. Without the sustainment structure, any 5S
will decay.
Kaizen is a philosophy of continuous small improvements, typically implemented through short
team-based events (1–5 days) that address a specific problem with practical, low-cost solutions.
Six Sigma uses statistical analysis to address high-impact, data-proven quality problems through
a structured 4–6 month project methodology (DMAIC). Kaizen is faster, lower cost, and broader.
Six Sigma is slower, more rigorous, and better suited to complex, persistent, high-cost quality
problems. Most plants benefit from running regular Kaizen events and occasional Six Sigma
projects simultaneously.
Yes. GreenDot offers a structured plant diagnostic — a shop floor walk, data review, and loss
analysis — that results in a specific, prioritised recommendation. This is always the first step
before any implementation. contact us or reach us directly at +91 90237 28317.
Ready to Choose the Right Framework for Your Plant?
GreenDot offers a structured plant diagnostic — a Gemba walk, data review, and loss analysis — before recommending any framework. We do not sell methodology. We solve operational problems.